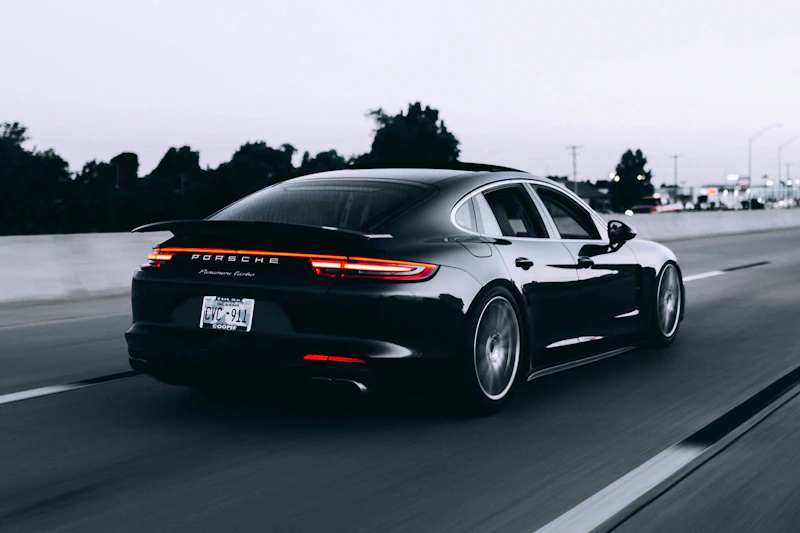
 Interior
Class A Trim Panels
Visible-surface interior panels with grain replication, moulded-in colour and zero-tolerance for sink marks.
Process 2K Molding
Material PC-ABS
Tolerance ± 0.15 mm

Twelve product families across four automotive domains, backed by the engineering services that get them from a CAD model to a validated part on your line.
Representative programs. Most parts we make are customer-specific and covered by NDA — these show the envelope we work inside.
Interior
Visible-surface interior panels with grain replication, moulded-in colour and zero-tolerance for sink marks.
 Interior
Load-bearing mounts and carriers replacing steel weldments, validated to full crash-load cases.
 Exterior
UV- and stone-chip resistant exterior parts with integrated clip geometry for blind assembly.
 E-Mobility
Lightweight housings with flame-retardant grades, integrated sealing channels and dielectric strength verification.
 E-Mobility
Overmoulded copper busbar assemblies holding creepage and clearance distances under thermal cycling.
 E-Mobility
Barriers, covers and interlocks for high-voltage zones, tested for tracking resistance and dielectric integrity.
 Thermal
Coolant distribution housings holding dimensional stability through repeated hot-cold cycling.
 Powertrain
Chemical-resistant reservoirs with integrated level sensing bosses and 100 % leak testing at end of line.
 Powertrain
Quick-connect couplings and routing hardware rated for continuous high-temperature service.
 Mechatronics
Moulded gear sets and drive components with controlled backlash and low-noise tooth profiles.
 Mechatronics
Thin-wall housings with moulded-in bearing seats, assembled and function-tested in one automated cell.
 Mechatronics
Overmoulded sensor carriers with sealed cable exits, qualified to IP69K wash-down conditions.
Most customers engage us before there is a part to quote. These are the services that surround the molding.
We join your program at concept stage, running design-for-manufacture reviews and tolerance stack analysis before geometry is frozen.
Full rheological, thermal and structural simulation to eliminate porosity, warpage and stress concentrations before tool steel is cut.
Soft tooling and bridge molds that produce functional parts in production material, so validation does not wait on the series tool.
Scheduled maintenance, refurbishment and engineering changes on tools we built — and on tools you inherited from elsewhere.
A single named engineer owns your program from kick-off through PPAP, with APQP gate reviews and open-issue tracking you can see.
Long-tail supply after series production ends, including tool storage, periodic requalification and low-volume run scheduling.
Specialised engineering and component manufacturing across mission-critical vehicular domains.
Validation happens on site. Nothing ships on a supplier's certificate alone.
| Test Method | Applied To | Reference Standard | Capacity |
|---|---|---|---|
| Dimensional / CMM | All molded and machined parts | ISO 1101 GD&T | 100 % |
| Optical 3D Scanning | First articles, tool validation | VDI/VDE 2634 | 8 μm |
| Leak & Burst | Reservoirs, housings, routing | Customer-specific | > 6 bar |
| Thermal Cycling | Thermal and HV components | ISO 16750-4 | −40 – 150 °C |
| Dielectric Strength | HV insulation, busbar carriers | IEC 60243 | 800 V class |
| Tensile & Flexural | Material lot qualification | ISO 527 / ISO 178 | Per lot |
| AI Optical Inspection | Class A surfaces, assemblies | Internal spec | In-cycle |
Share a 3D model and target volumes. You will get a manufacturability review and an indicative quotation, not a brochure.